Showing posts with label dropouts. Show all posts

Wednesday, 16 April 2014

Fork it

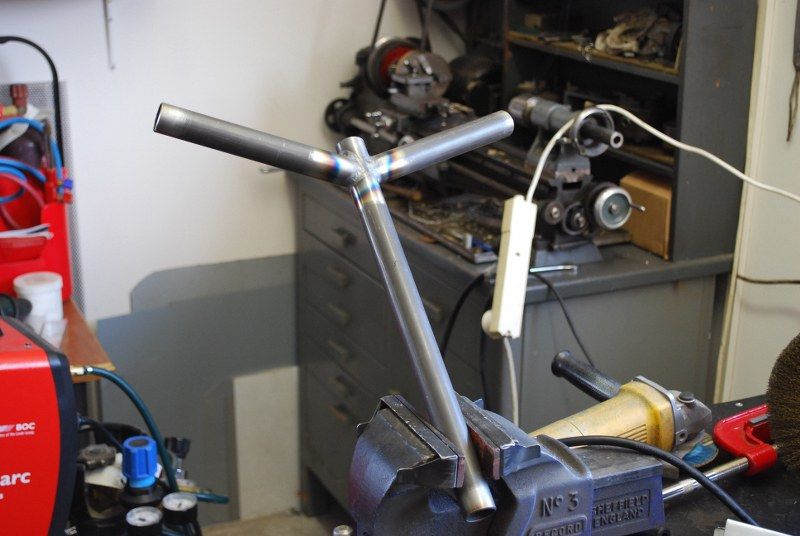
I may have mentioned that I was not 100% happy with the forks on the Fatness, the biggest issue being the steerer tube flexing quite disconcertingly under load. This was because I used straight gauge 4130 where I should have used a proper butted tube. Various tiresome things have got in the way of doing anything about it, but now things have progressed.

One of the issues preventing progress is that I was really quite unhappy with where my TIG welding skills were at. I started the new forks a few weeks ago, but the welding of the crown parts to the steerer was frankly terrible, with lots of bubbles and voids and large chunks of tungsten thrown into the mix. I could TIG weld once upon a time, so why couldn't I do it now? This stalled things because I want 100% confidence in something as stressed as a fork and I fell into framebuilders funk.

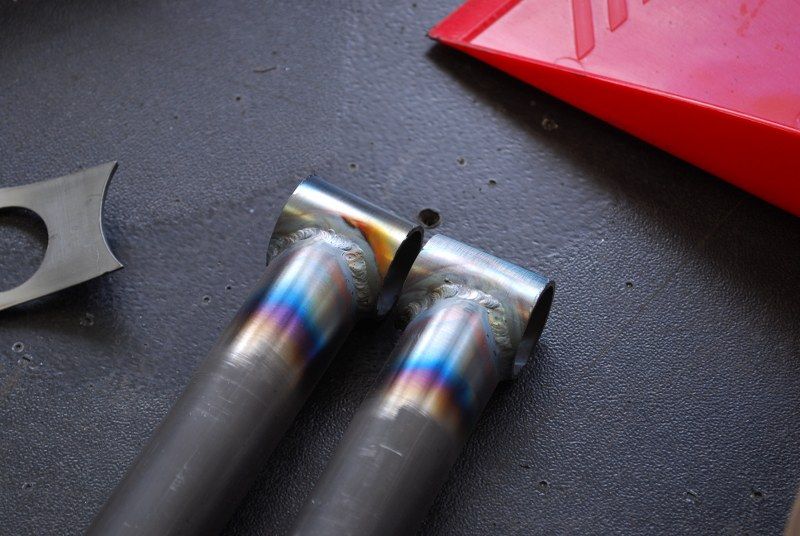
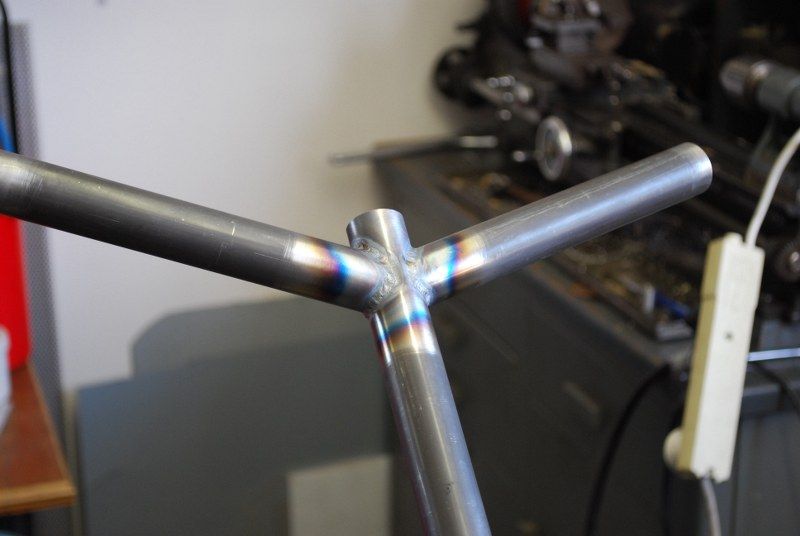
As it happened I had ordered enough parts for two sets of forks, so a few days ago I decided to start in fresh on the second set. I did a few trial welds with the same issues, then decided to swap the tungsten from the recommended thoriated type to a ceriated one that came with the machine. What a difference! It was like coming home and settling in front of the fire with a hot toddy. And so I cracked on with super renewed enthusiasm. The skill is still not at the level it was when I did it for a job, but it is way, way nicer than it was.

Mitering in the fork tubes
Some slightly better then previous welds, yesterday. The next ones were much better than this.
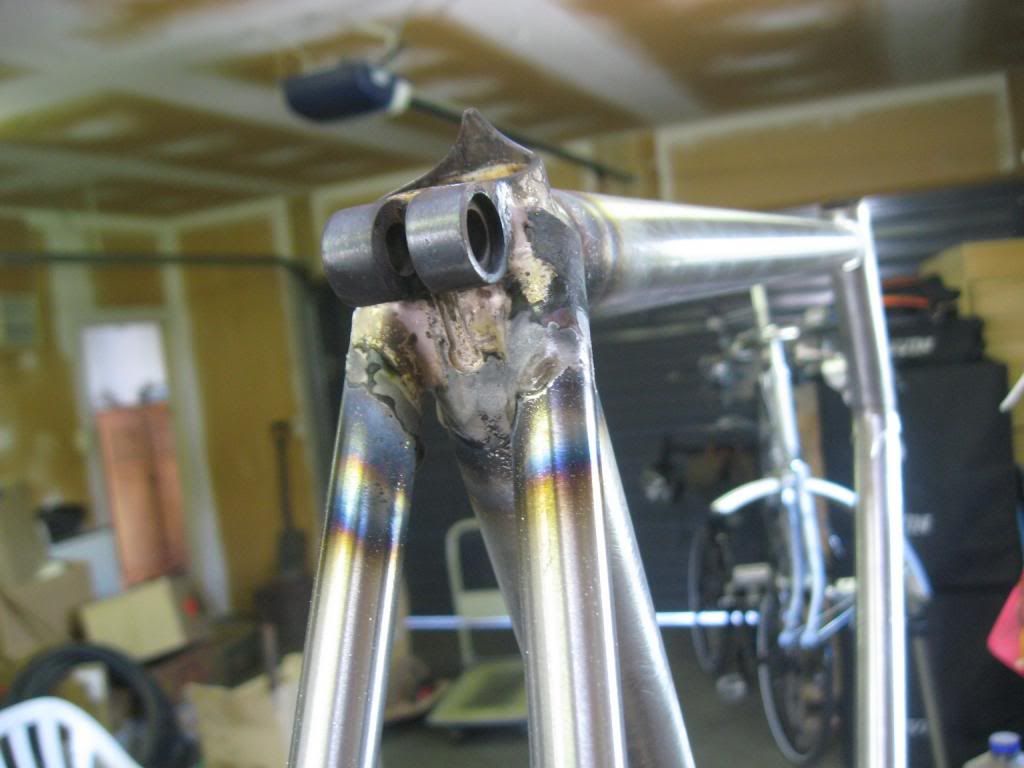
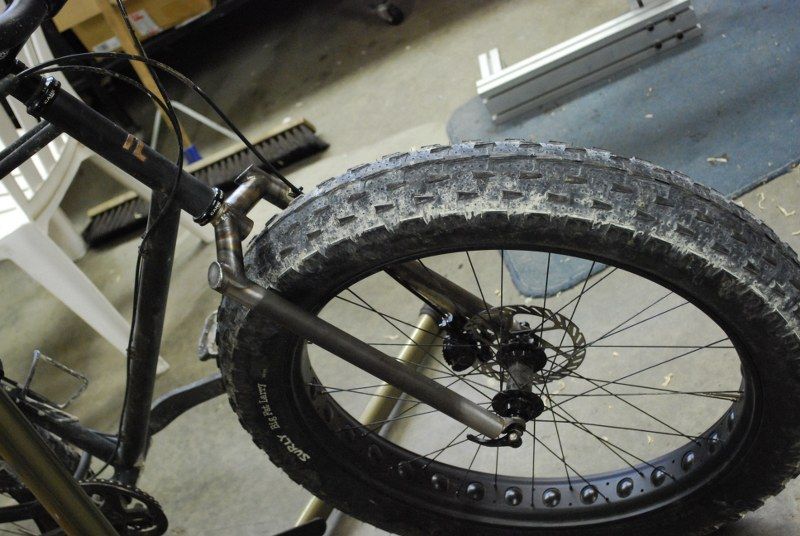
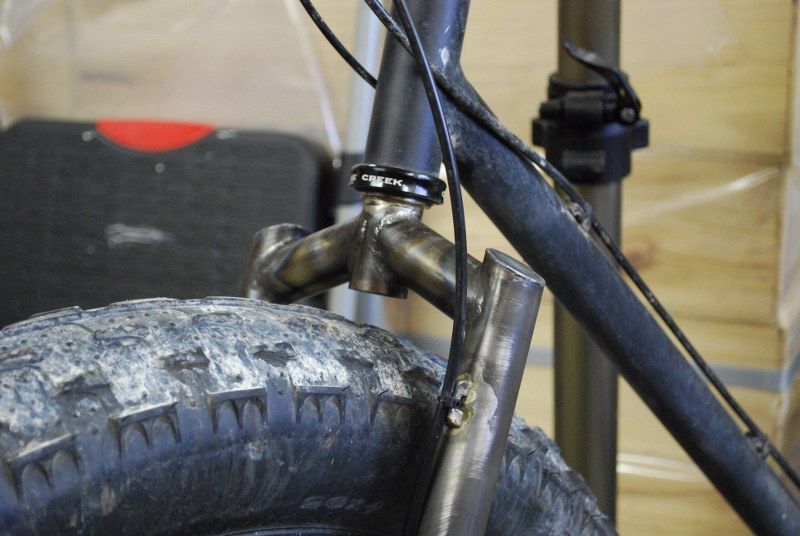
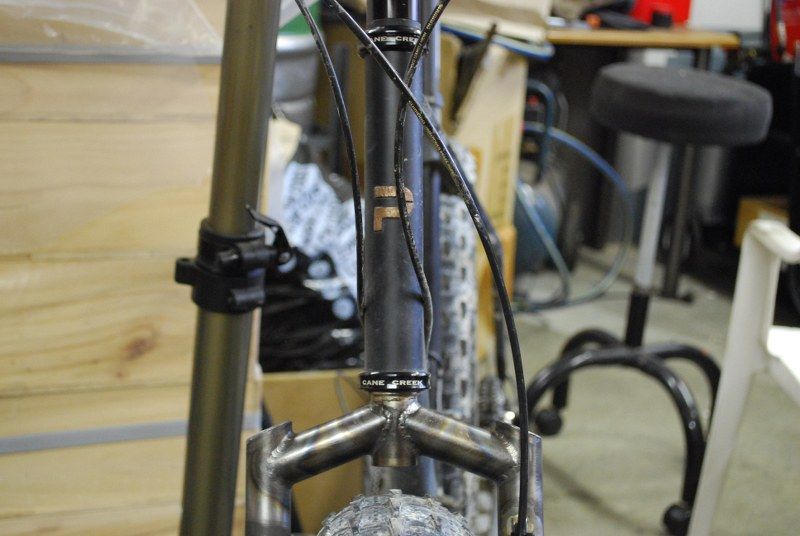
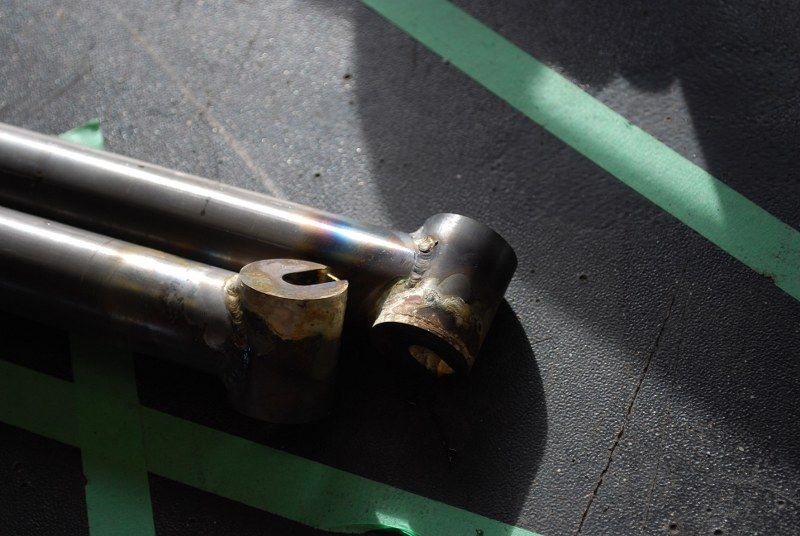
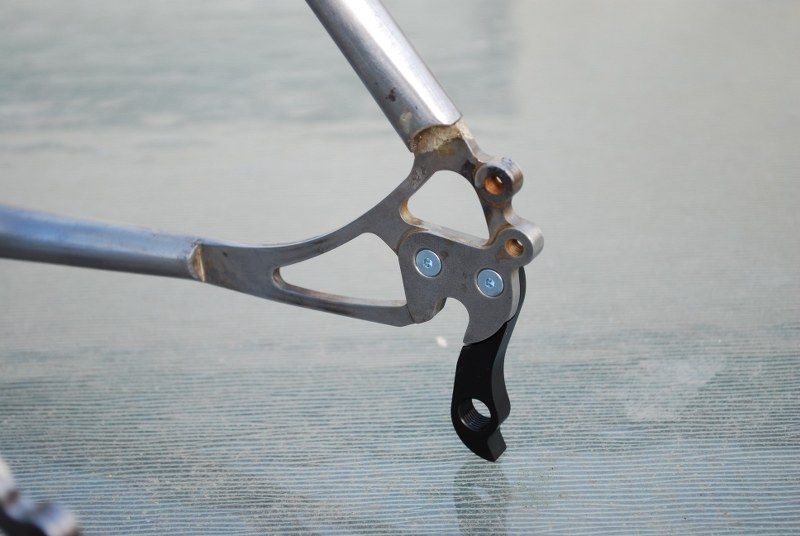
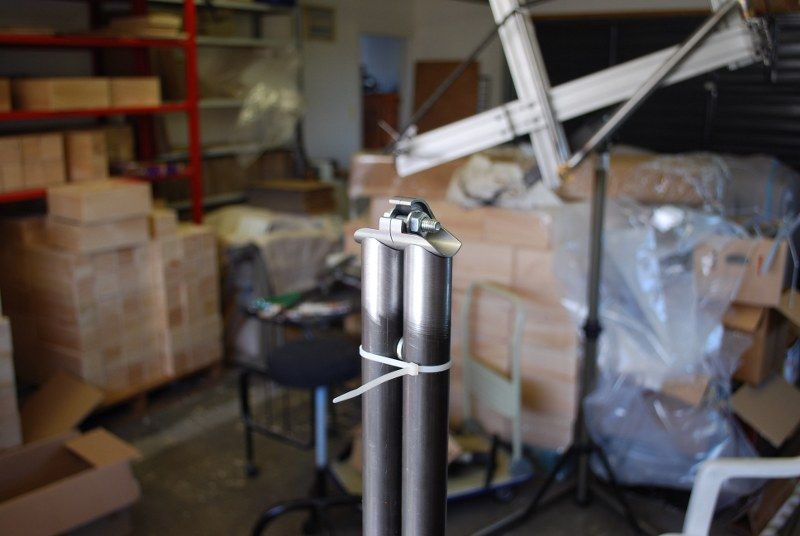
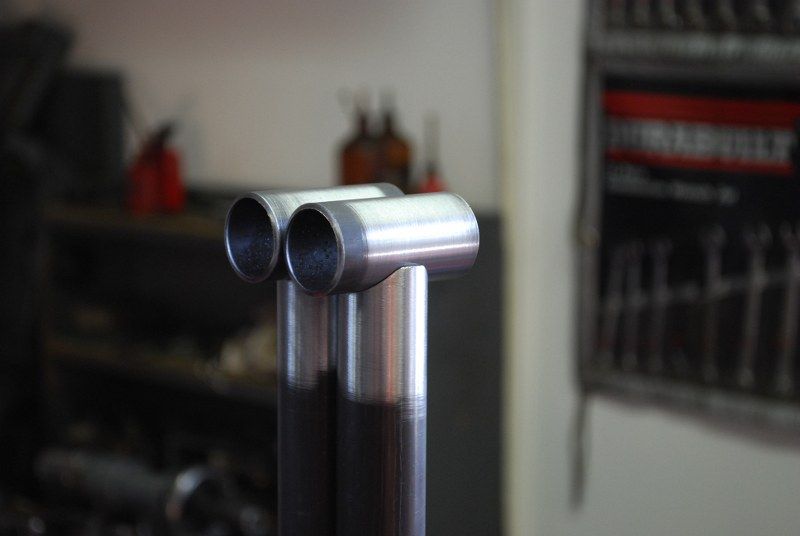
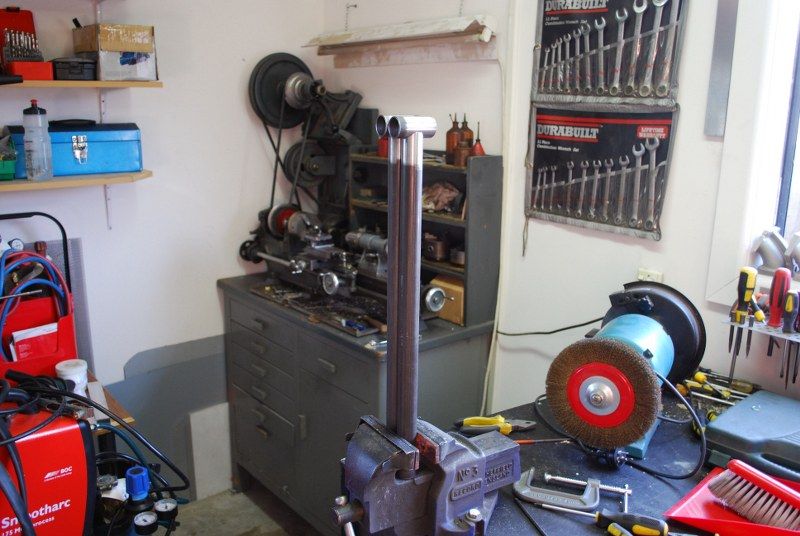
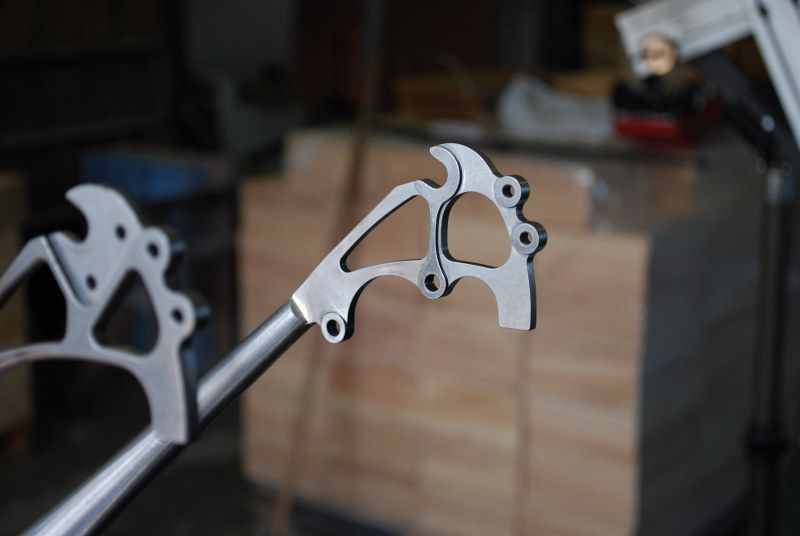
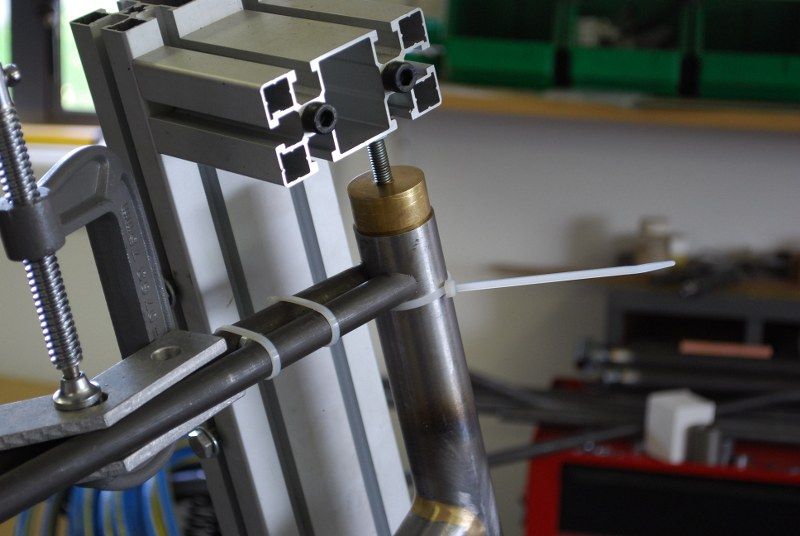
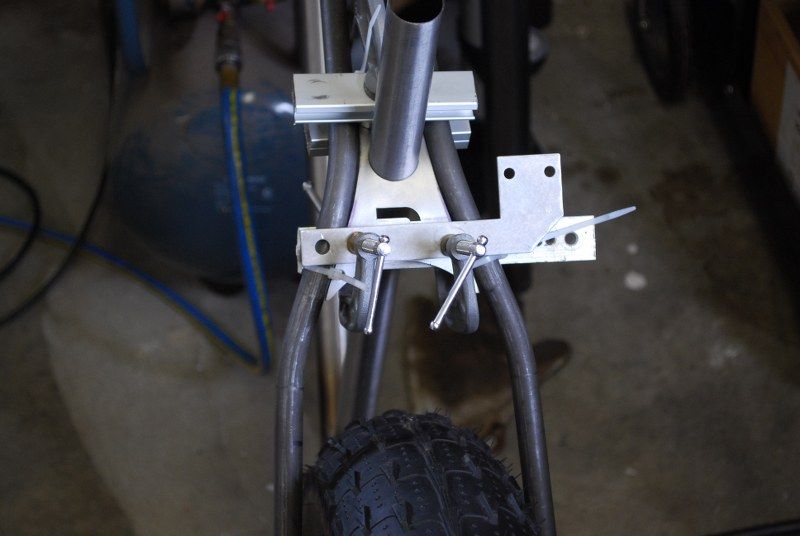
All fitted up. I changed the design detailing a bit, the fork tubes are closer to each other for a start, this was defined by the Ceeway sourced plug in dropouts I used.
The fork is also taller to give a bit more vertical clearance. This slightly slackens the headtube angle, and I took a 10mm spacer out of the stem stack to drop it back to the previous height.
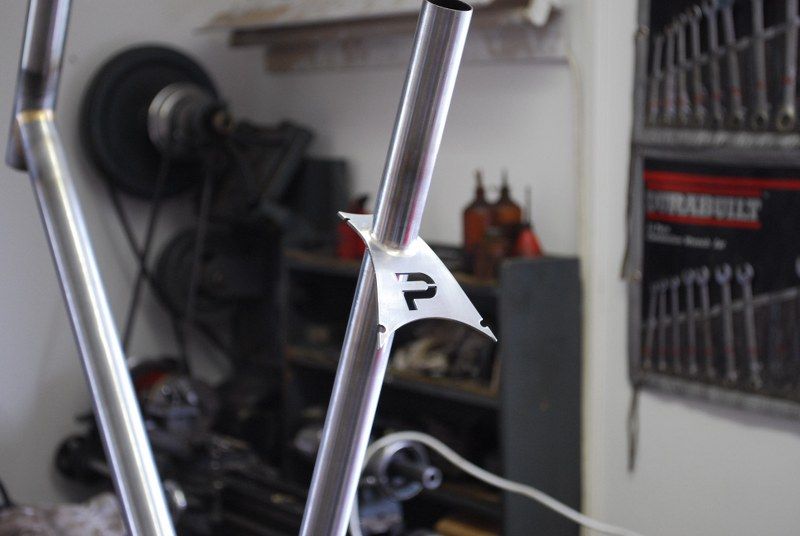
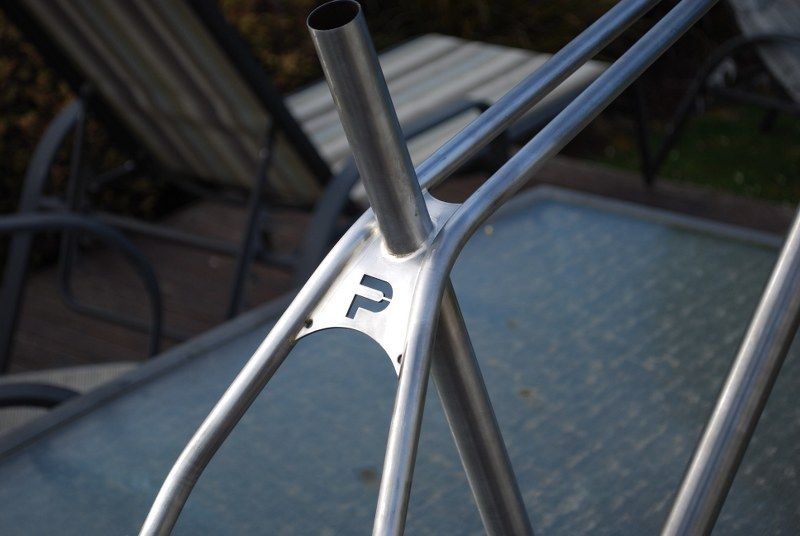
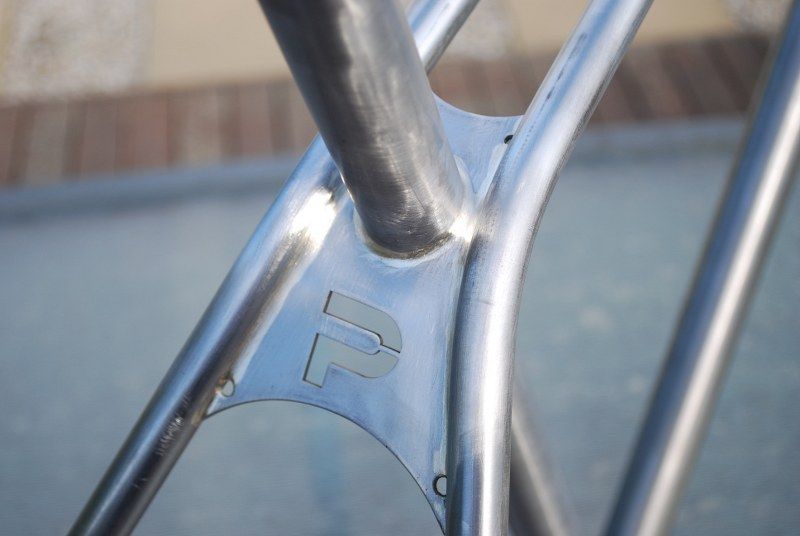
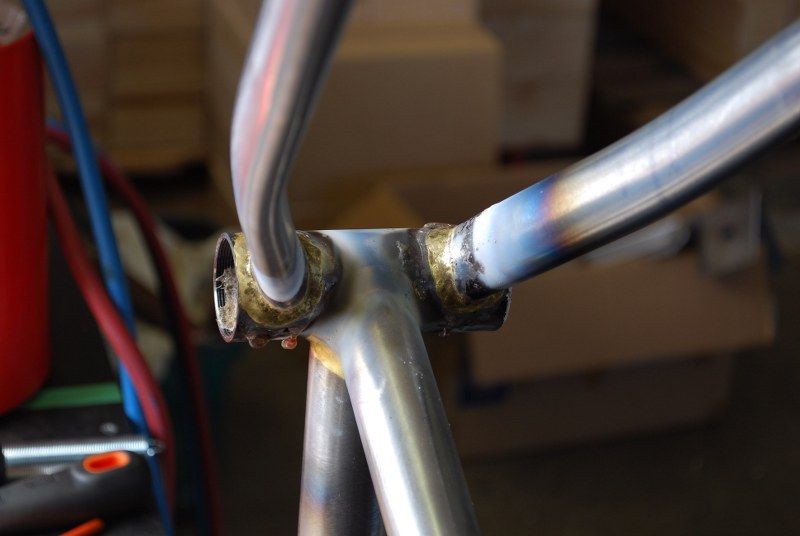
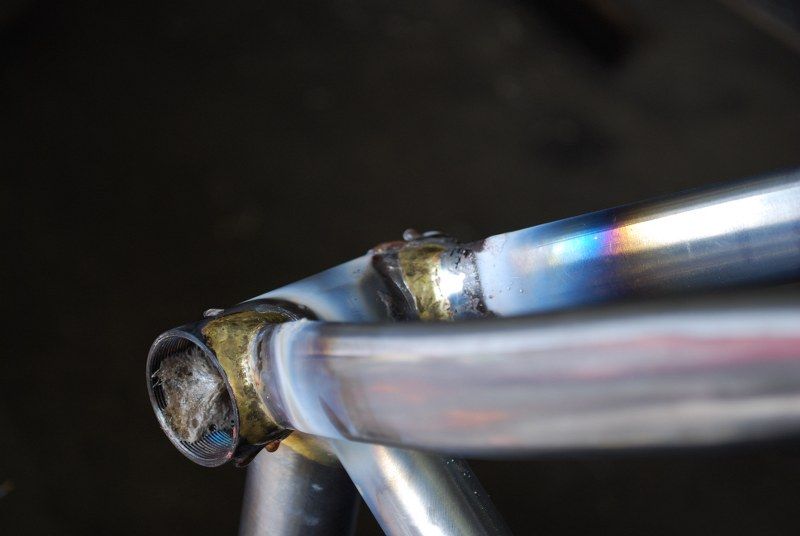
And I angled the fork tube caps and used flat sheetmetal instead of coins
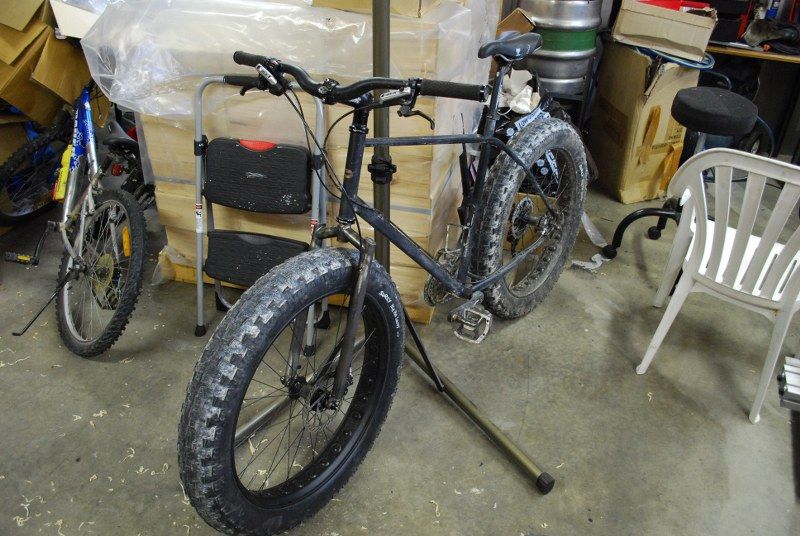
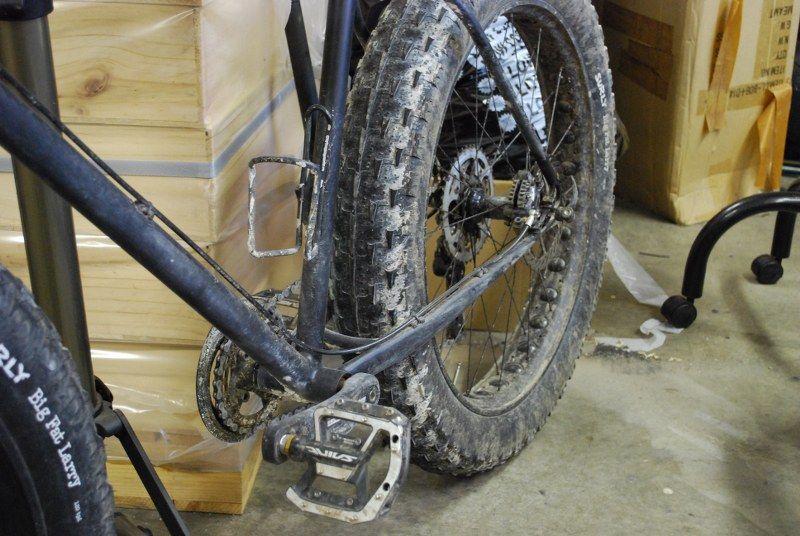
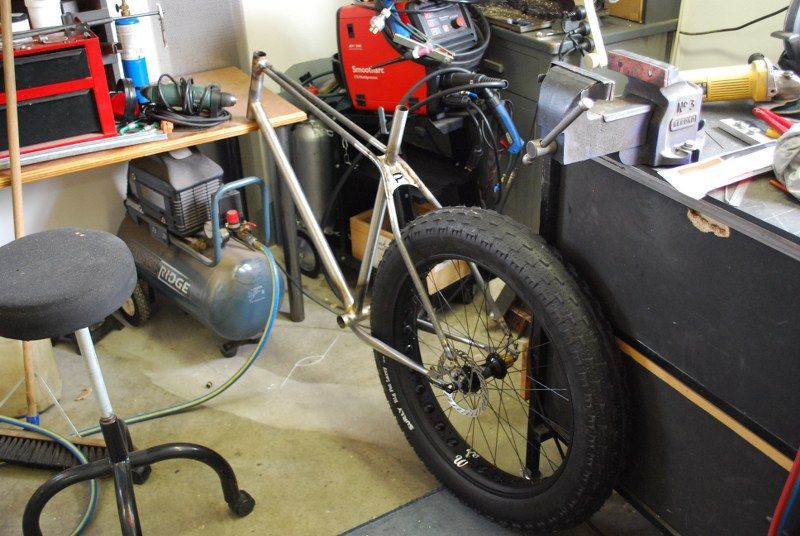
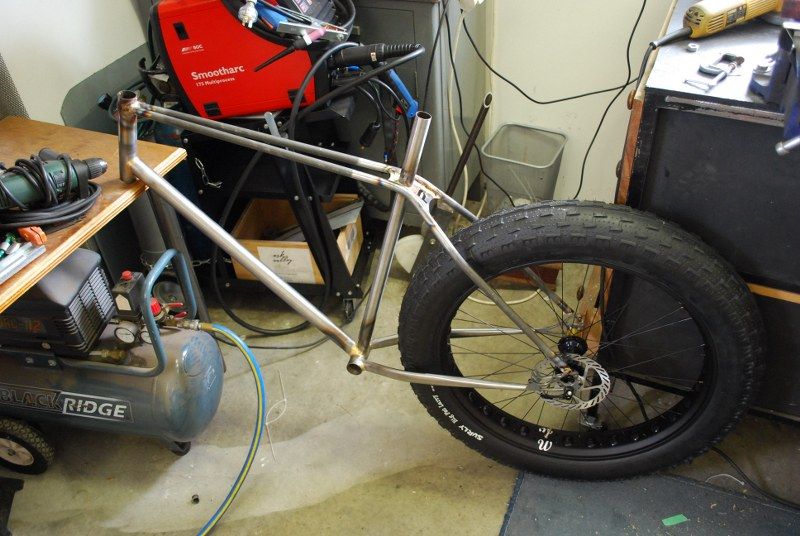
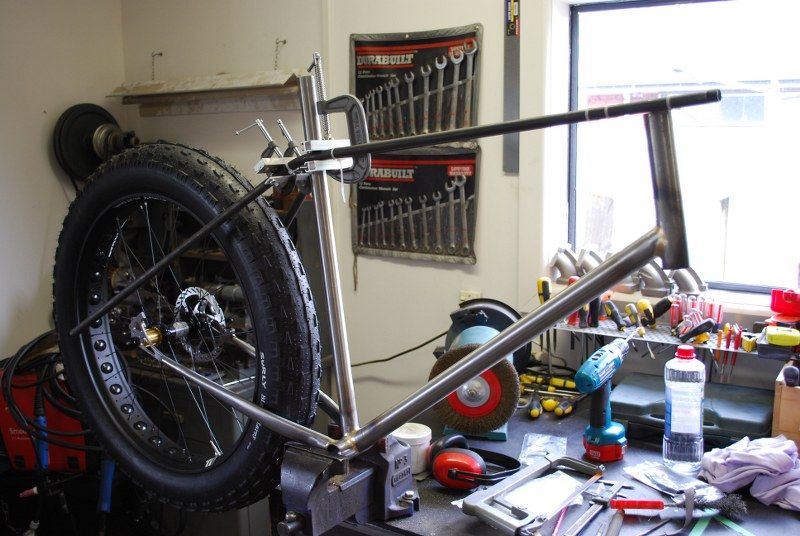
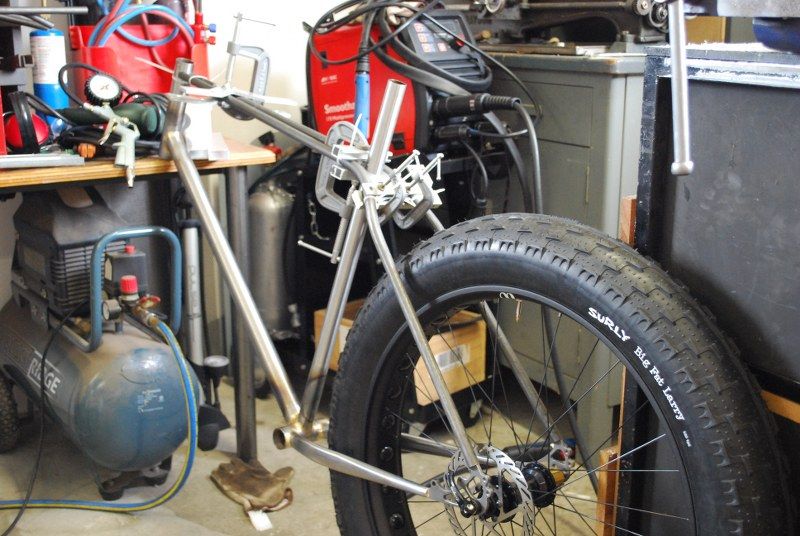
Well, it is a fork attached to a fatbike. Time to see if it will work....
Yes, I have been riding some wet trails in the recent past. All trails in Christchurch are wet and will be for the foreseeable future.
So the plan is to ride it as it is for a week or two to see if there are any niggles, then strip it down for coating. The thin coat of primer is not really cutting it in the current conditions. I have been riding it a lot though.... including a trip with some fat friends to Hanmer.

In other bike related news I built this up for my eldest daughter - I got sick of buying crappy kids bikes and I figured this would last her for a good long while. I got it as a stripped frame and forks with wheels and brake calipers. By the time I bought a headset/BB/chain/cassette/hanger/derrailleurs/discs/levers/shifters/tyres it became probably the least economic option possible. But it looks sweet and will last forever. She loves it.


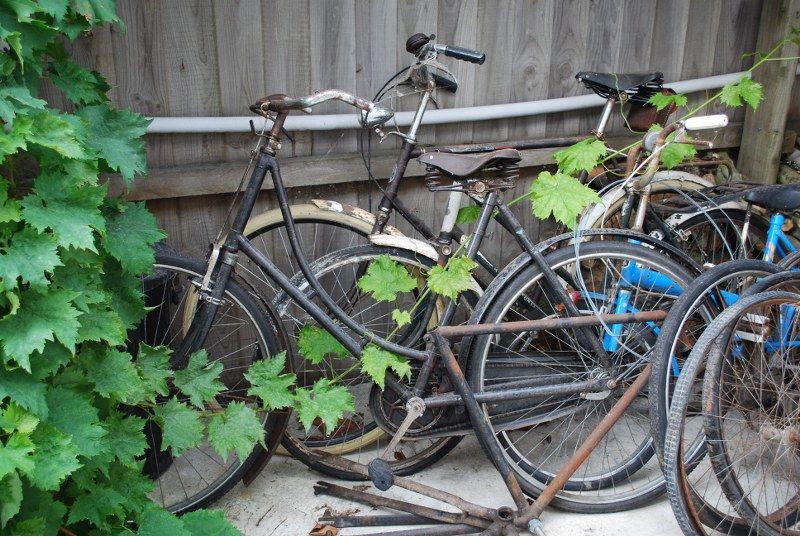
I also spotted these forlorn looking beasties in the woodshed, I will need to bring them inside for the winter I imagine.


In other, other bike related news I have a new set of tubes awaiting me in the garage. These are to make into my wife's fattie, which I may well TIG now, and looking further out I have plans for an updated commuter with disc brakes and much other secret goodness.

Sunday, 24 November 2013

The Mistake Free Top Tubes MkIV™

I have pretty much been in the garage every night this week and nearly all of the weekend, so things are moving quickly...

My extra tubing arrived on Tuesday morning, allowing me to utilise lessons learnt from the tube bending learning curve to great effect. In a couple of days the tubes were ready with minimum fuss and no obvious mistakes. But first the forks, which stretched the limits of my TIG skills.

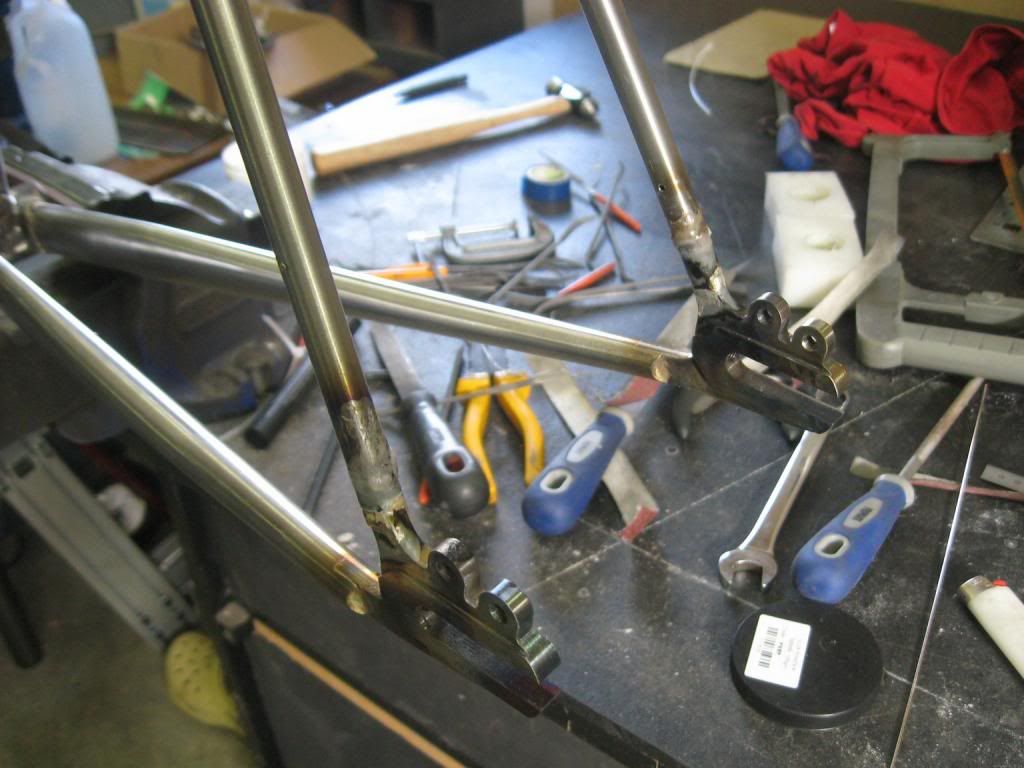
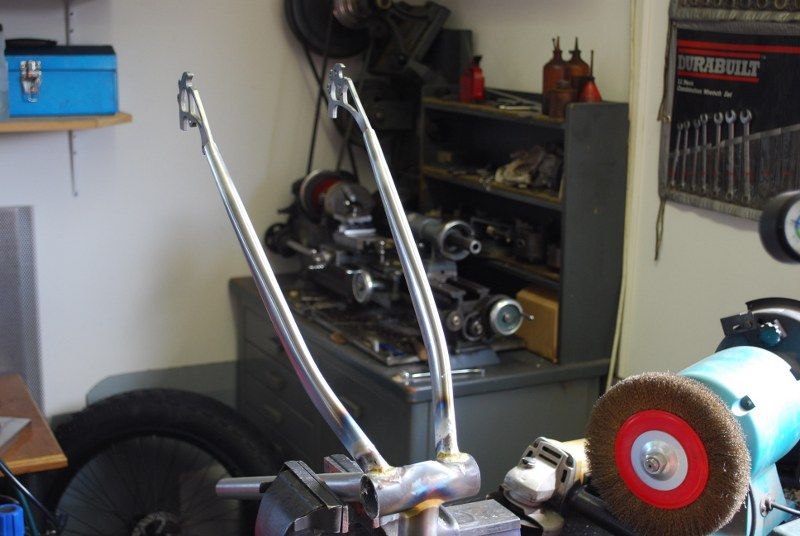
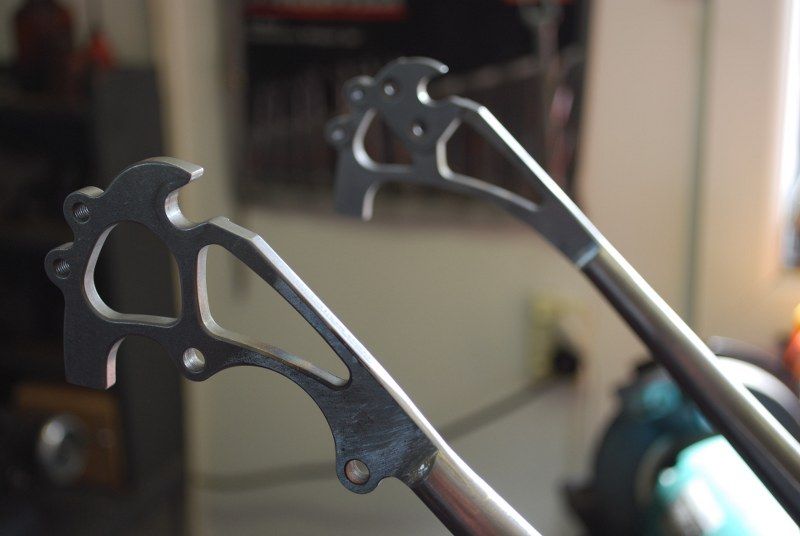
I re-used the actual dropout bits of the Paragon failure, mostly because I didn't have any other suitable material lying around. The dropout holes are not at the same centers as the tubes so turning them down to suit what I had required some thinking and setup on the Grayson. Here they are freshly silver soldered into the leg tubes.
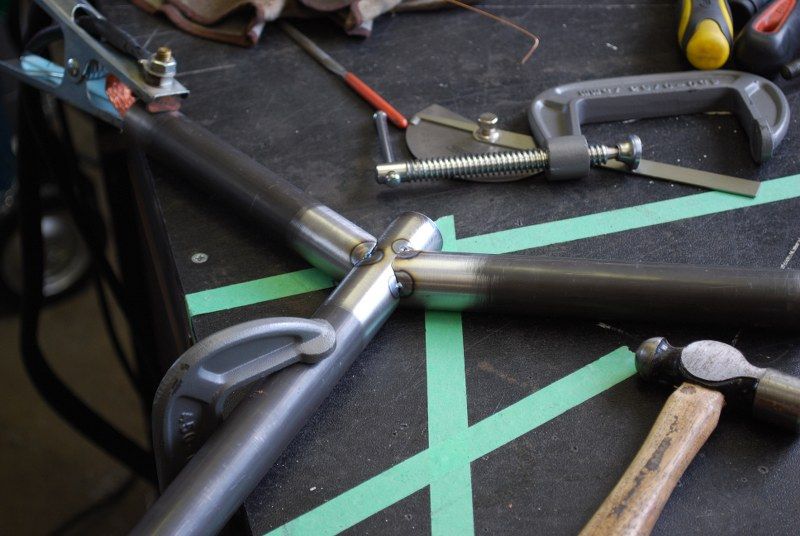
Much time was spent taking microns at a time off the leg tube to crown miters, I have learnt the hard way to take this sort of thing slowly, and I get slower when both bits have required some effort to get to a level of complexity. I then welded it up but forgot to take pics.
Mistake Free Top Tubes MkIV™
The Mistake Free Top Tubes MkIV™ come free with several meters of randomly badly bent tubes, sort of like steak knives but less effective for slicing vegetables. I clearly need to design a frame that utilises many many very short bits of straight pipe.
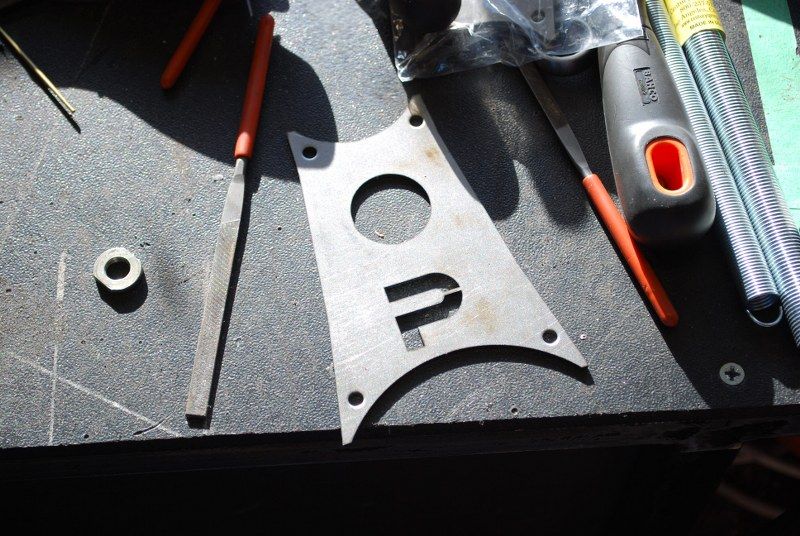
Once I was basically happy with the top tube mitering etc I brazed in the top plate. This was silver soldered actually as it is such a beautifully controllable thing to do and I did not want a big fat braze in there. As things were going to be a tight squeeze in there I cleaned it up nicely before getting too much further down the track.
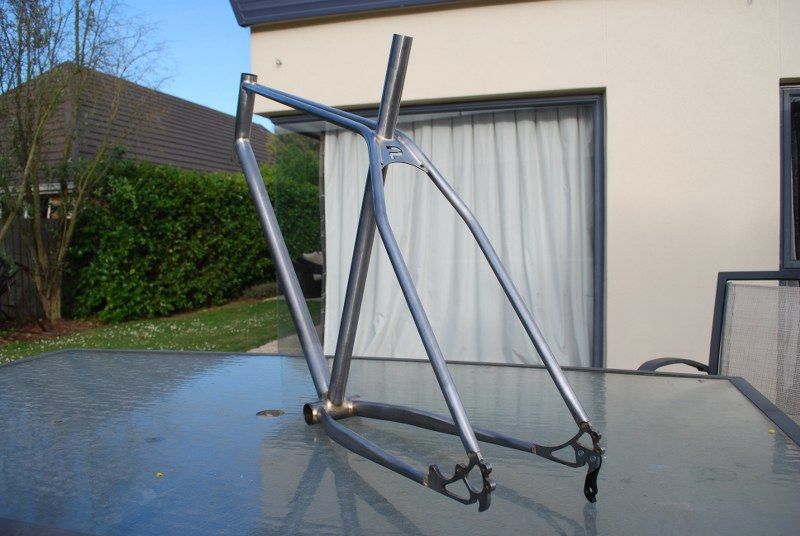
I then fettled the fitment of the The Mistake Free Top Tubes MkIV™ so they slotted into place beautifully. Clearly some things just require you to bollox them up a few times before you can achieve creamy goodness.
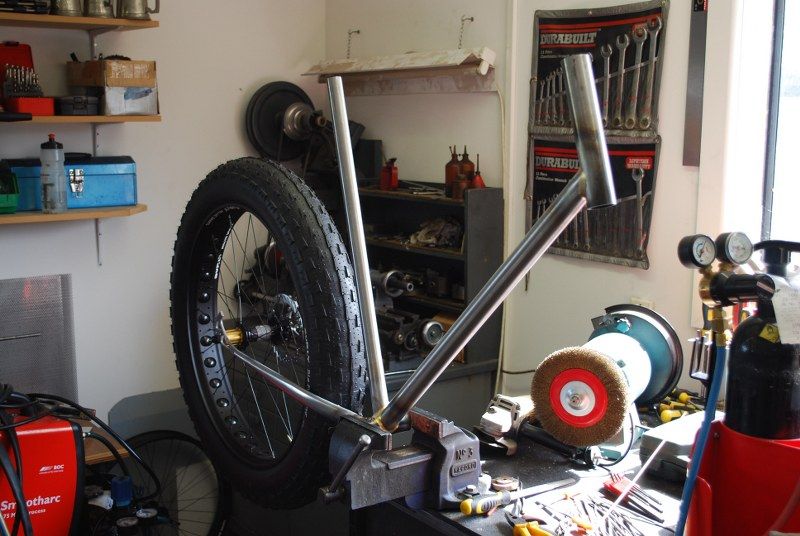
I then plunged into welding the things into place and before it was even cool I had to chuck the wheel in to see if all was well, which it was. The dropout slots will require some very minor loving to get the wheel sitting 100%, but it is looking pretty good as it is.
It looks so much better with those bends tucking around the wheel.
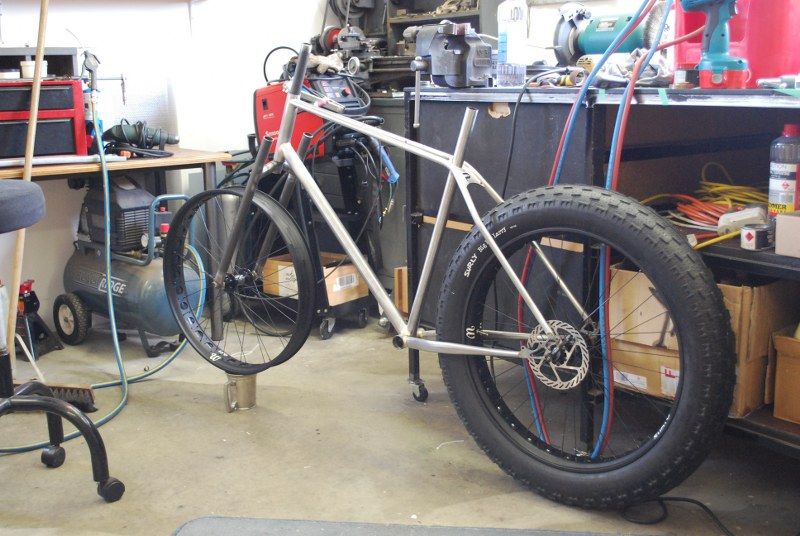
And then I thought I would chuck the half finished forks on to see how things shaped up, unfortunately I only have one tyre at the moment. An upside down pewter tankard is an admirable tyre replacement, but it might make for a slightly bumpy ride.
I spent some time today cleaning things up, there is still a good few hours yet to spend though.
I have made a bridge to fit in here but I need some more silver solder rods before I can do any more.
Some nearly finished fillet brazed cleanup.
This plate ended up with a bit of a shave off the sides, I think it still works visually.
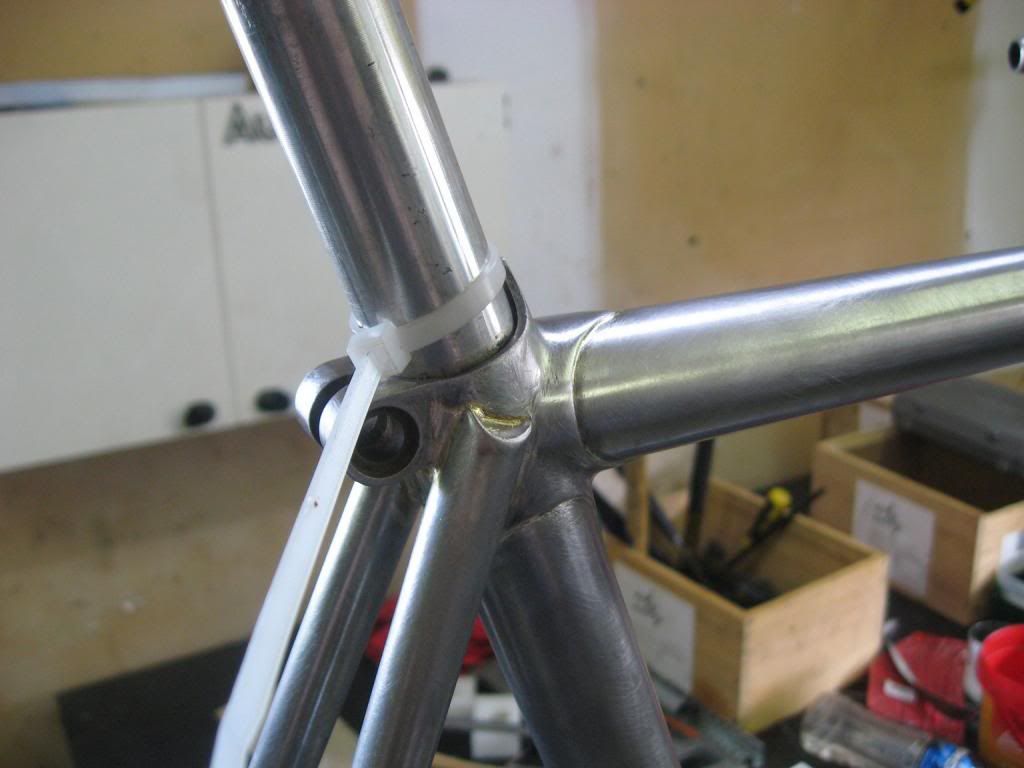
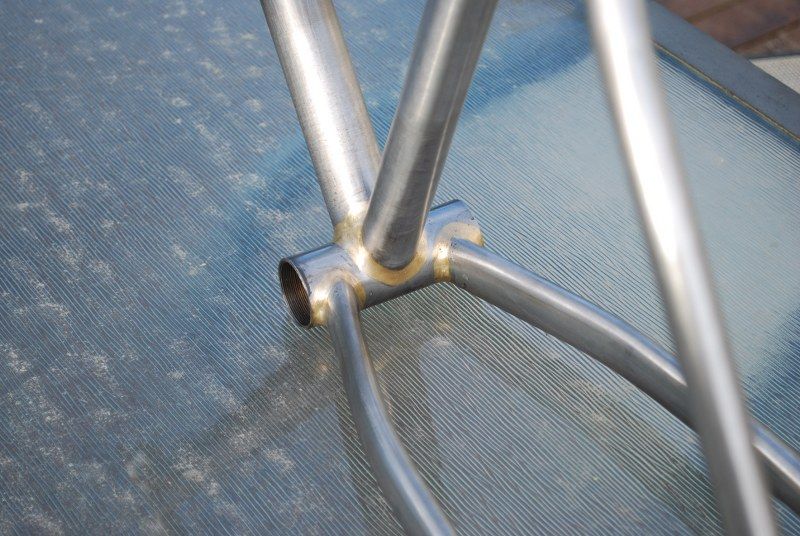
I have silver soldered the seat stay joints and sweated the filler up inside the junctions, I will clean up and cap the open ends a bit later when I have more welding rods.
This pleases me.

I am discovering that at the end of a build session I get a certain feeling depending on how well or badly that particular bit of the build has gone. If it has gone well it means that I have been in the zone and doing things that I am totally comfortable with, without rushing or stressing. Then I get a warm glow of satisfaction...

 If I have rushed or stressed then I am clearly not in the zone and I end up with a knotty feeling centred on my solar plexus, reminding me that I did not do as good a job as I could have when making that particular bit. I am getting much better at stopping or changing what I am doing until I am in a better space.

My current aim in life is to build a frame that is the culmination of build sessions that have all ended in the warm glow of satisfaction. This may take time and a number of frames.

Yay.

Saturday, 16 November 2013

Frame Rate

I must say that fillet brazed frames go together a lot faster than lugged frames. I have spent a good few nights and weekends working away at this, and apart from the twin top tubes which have proven to be a bit of a pig, this have moved well. I have also decided that I should care more about photography so have been using my fairly nice Nikon rather than my cellphone. This means I have taken far too many photos, many of which are in focus;

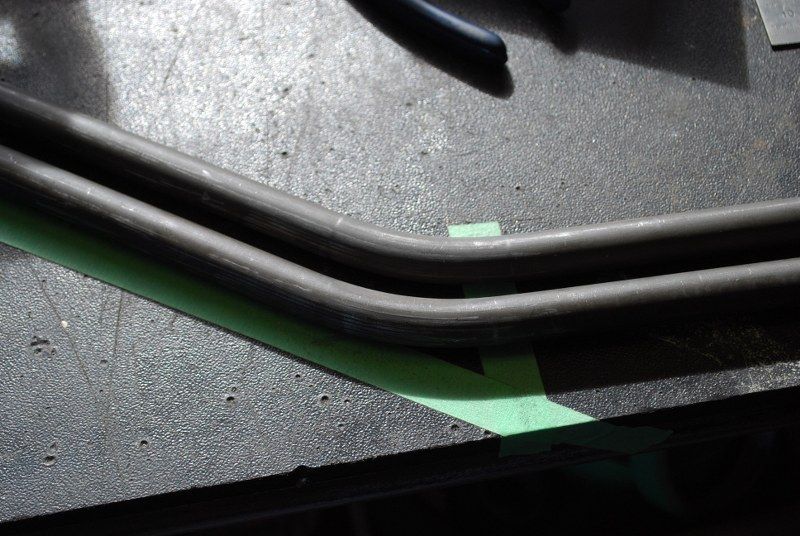
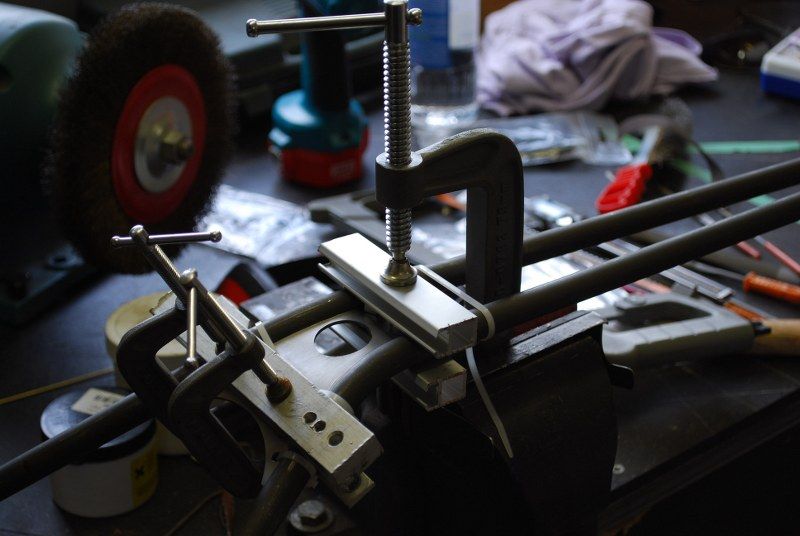
Two lovely tubes, I have finally nailed the bending process probably

The start of many, many fitups of those bloody top tubes
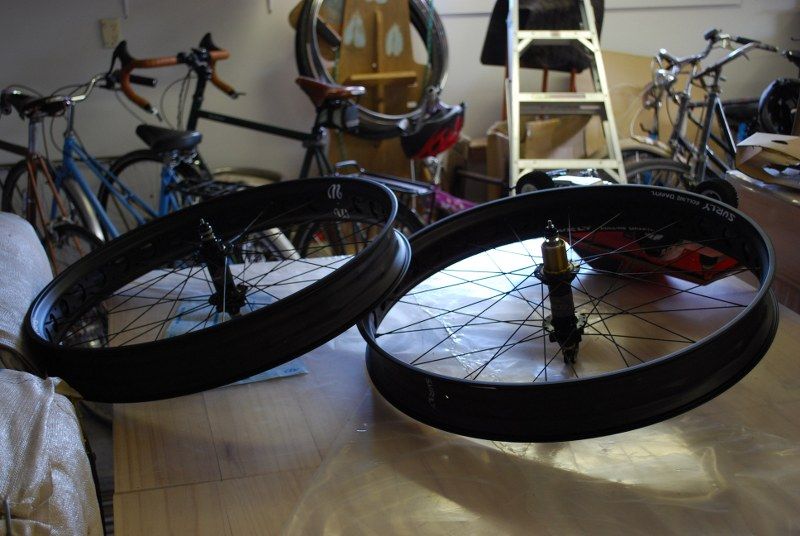
The wheels arrived - yay!
I started the forks using Paragon dropouts, unfortunately my TIG skills are not yet that great and they ended up too untidy to use, hence;
The start of my fully custom front dropouts.
Fork legs
Brazing the chainstays
More chainstays
The outside fillet on both of these had a bit of porosity, I had to grind it all out and redo that bit, I am not sure exactly why this is so as I made sure things were clean. Maybe not clean enough...
Rear dropouts from Paragon, I silver soldered these in.
Check out the mad photography skillz - depth of field yo
Fitting up the rear wheel to see if it fits at all
Hard to get lots of clearance with Big Fat Larry 4.7" tyres!
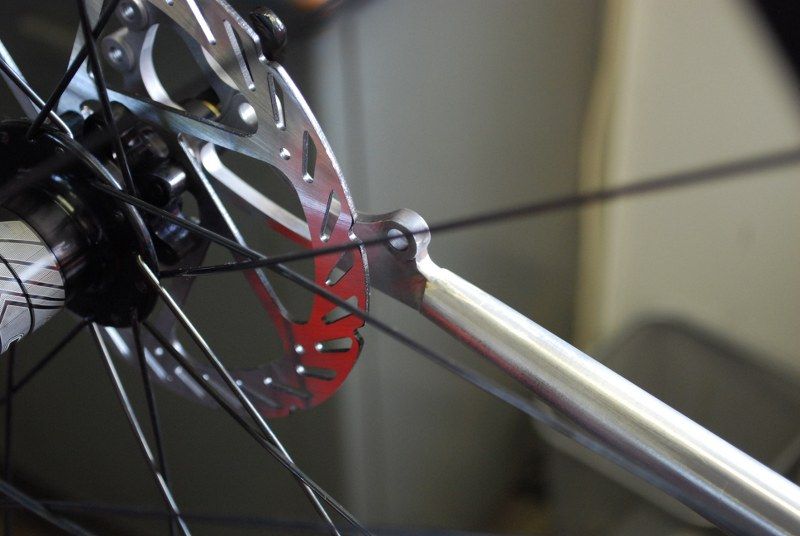
I checked the brakes all lined up as well
I got this laser profiled for the seat plate
I bent it up and jigged it in place, it was immediately apparent that the tubes were sitting too wide, so I rejigged it all with a fair bit of width taken out.
Endless fitting up and checking before I made the first cut of those hard won tubes
But then I bit the bullet and mitered in the front
Now just the back bends to do
Back bends achieved.......but
I am just not happy with how the lower bends ended up, I wanted them to tuck right around the tyre, but through a slight (yes again - I know) miscalculation they ended up there. I am sure they would be alright, but I suspect I will be allowing Leanne to retire just that bit sooner on Monday.
So I cracked on with the forks...
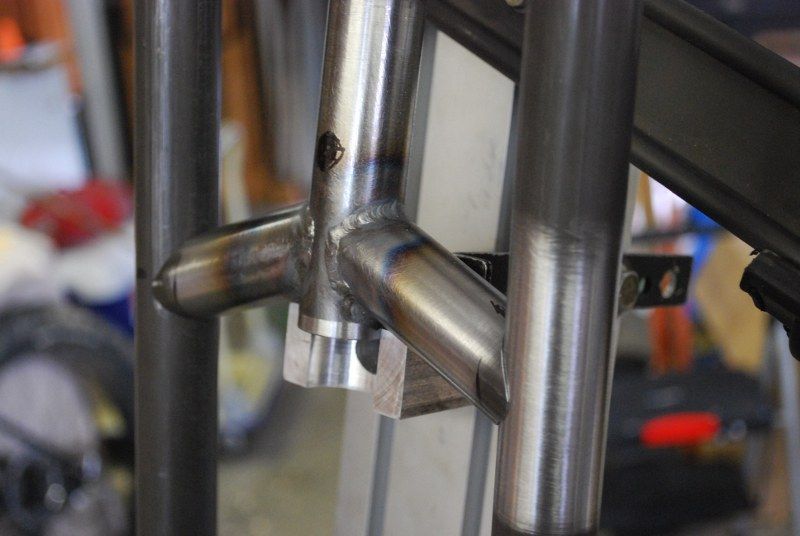
TIGged the dropout tubes - not yet perfectly tidy but I am getting better every day.
TIGged the crown tubes.
I made sure there was a good overlap of all the fork joints as burning away the edge of the tube end was my downfall when welding the Paragon dropouts.

Saturday, 16 February 2013

A wild Bicycle appears

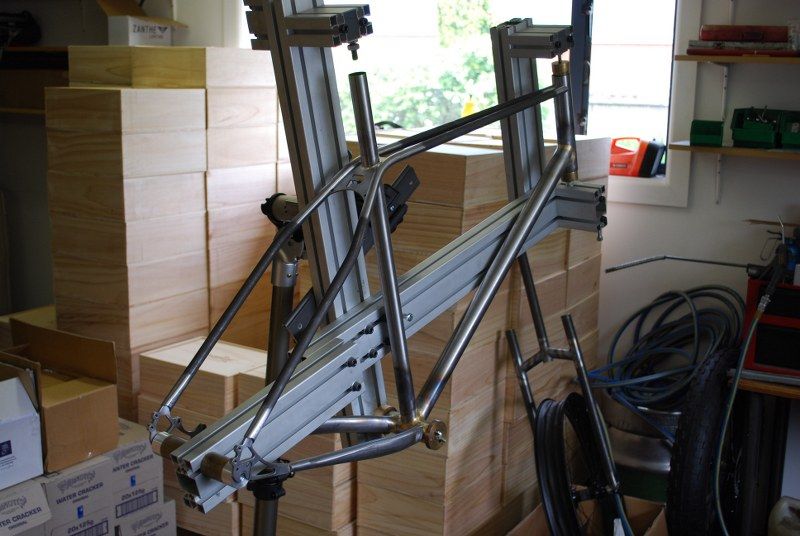
Having done nothing for a month, the tables have turned and I am now flying through the work with amazing speed, meaning the frame is basically complete except for the brake bridge, chainstay bridge and the brazons. I have decided not to split the seat stay for the belt drive now for a few reasons, but mostly because it would have stopped the momentum I have built up...

One thing I did this week was to check the frame geometry against the Surly, and surprisingly the two frames are almost exactly the same apart from the top tube height, the Surly being 1cm lower. This is quite pleasing, an hopefully means that I made the right decisions when I designed this frame.
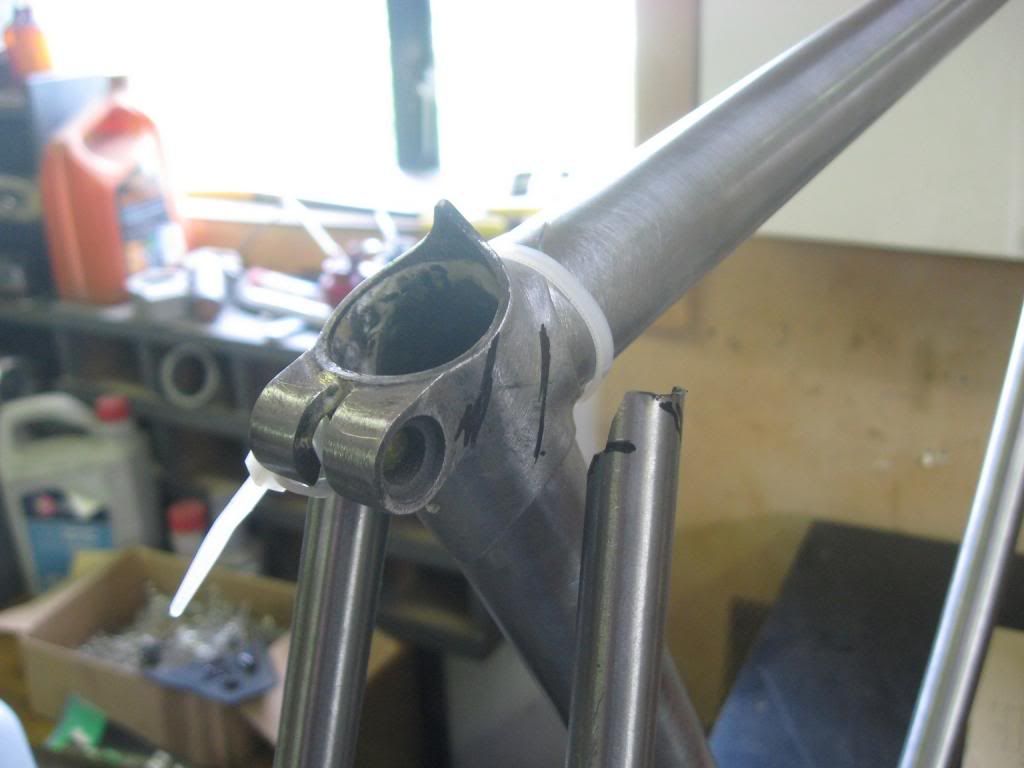

Sorting the seat stays
Brazing the bottom of the seat stays
Brazing the top of the seat stays
Pretty much done :-)
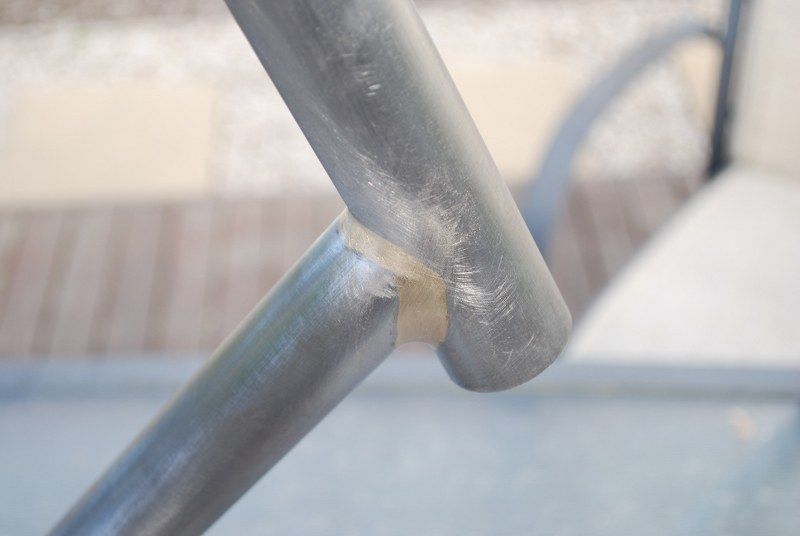
Mostly cleaned up - I decided to just keep things simple with the top of the seat stays and replicate what I have done with the dropout joints.
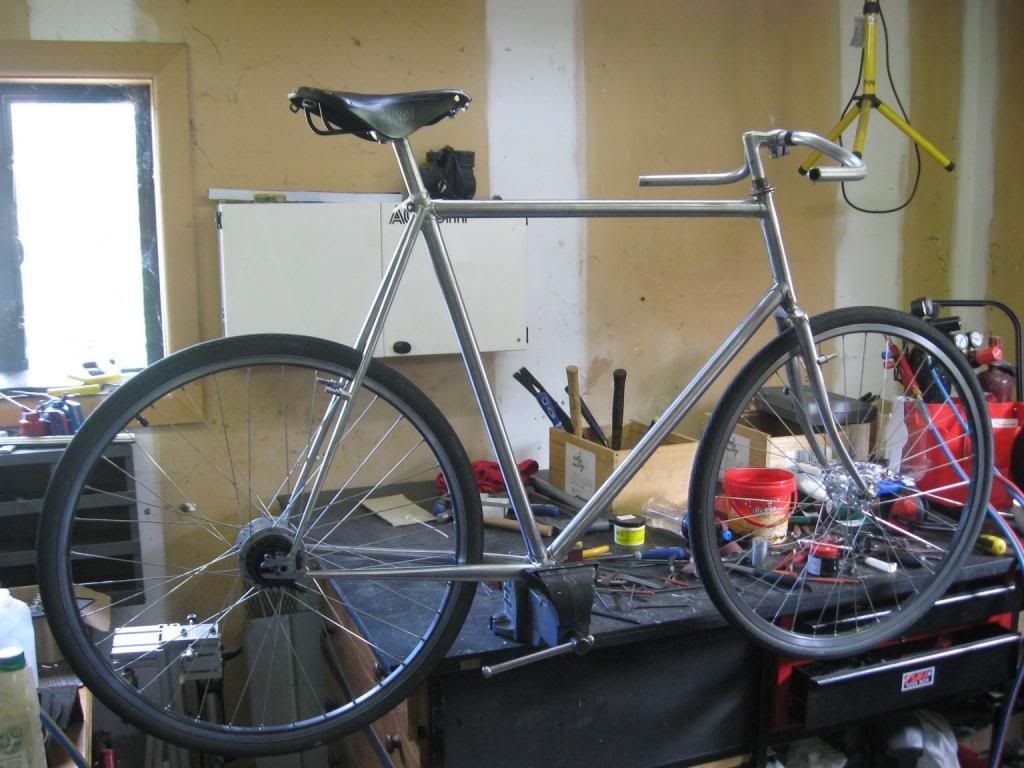
I got so excited I decided to mock it up - OMG a wild bicycle appears!
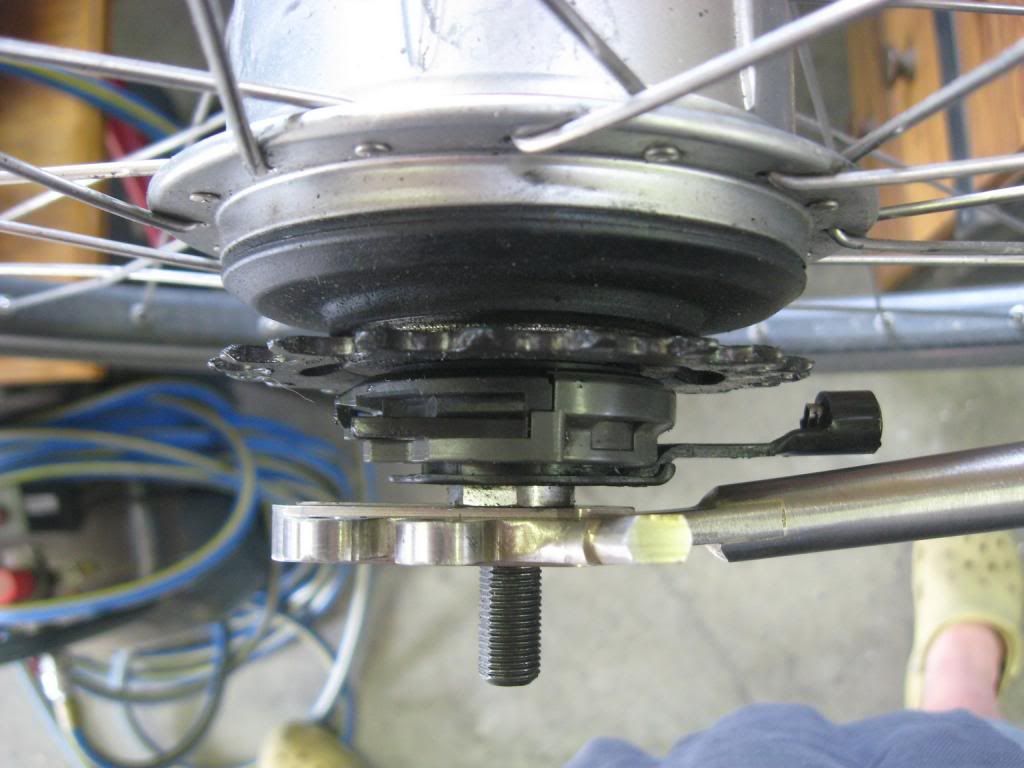
Plenty of room for the Alfine mechanism
Still some fine cleanup work to do on all the lugs...
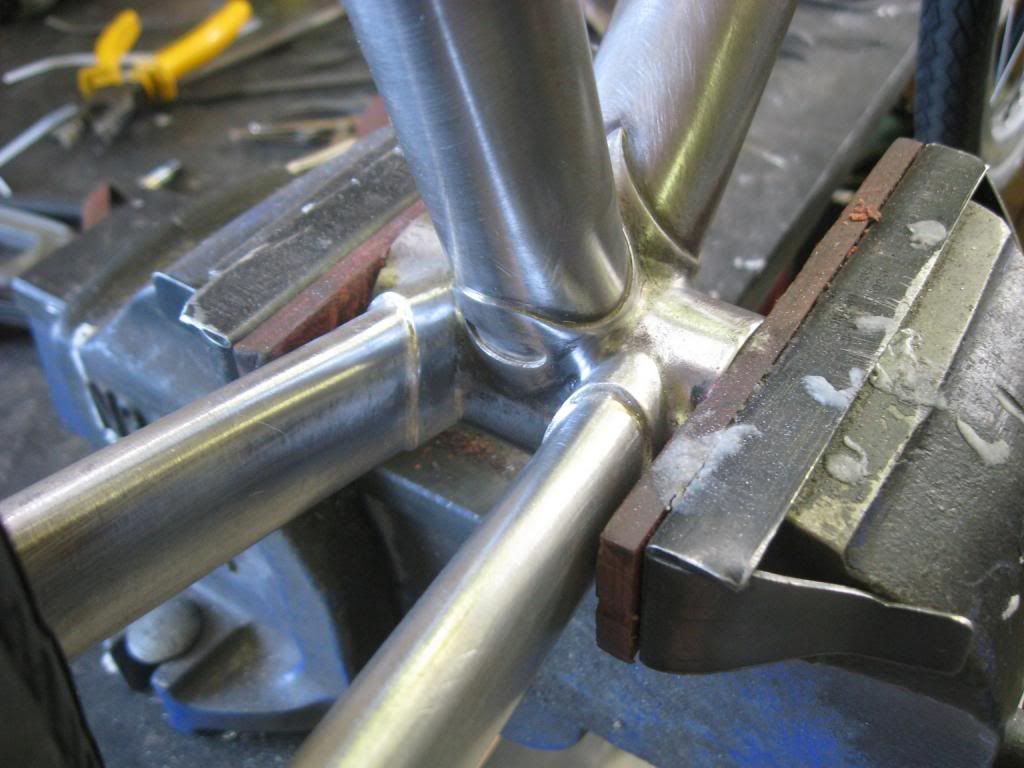
A recently brazed bottom bracket.

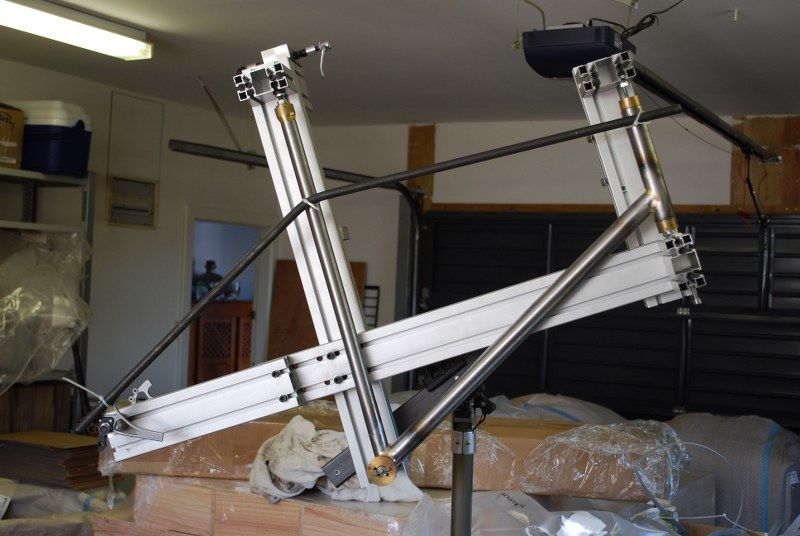
As I was so into the actual making I failed to take a lot of pics and did not document some of the important things that happened. One of these was cold setting the frame. After I did the head tube to down tube joint I pulled it about a bit with a long bit of pipe to make sure the angles were still the same after welding. I also did this once that assembly had been brazed into the seat tube/bottom bracket assembly. This is to make sure there are as few pre-stresses as possible in the finished frame, which would make the chances of it pulling things a bit wonky much greater.
--------------------------------------------------------------------------------

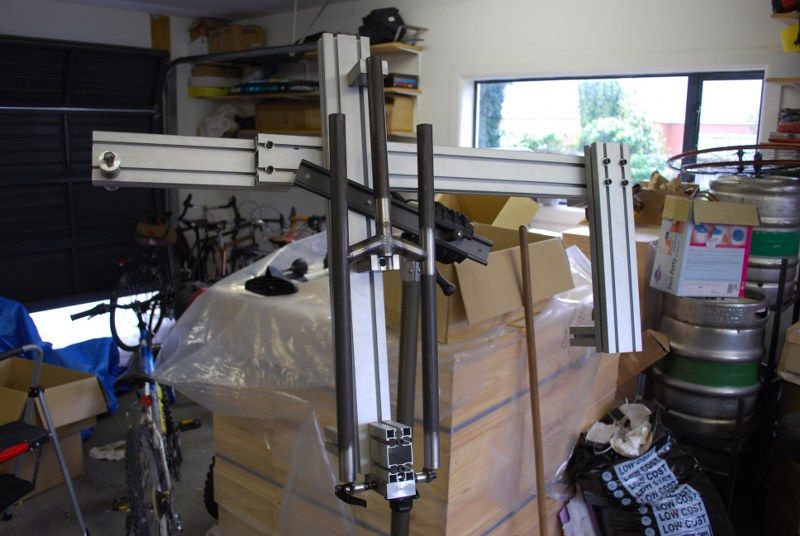
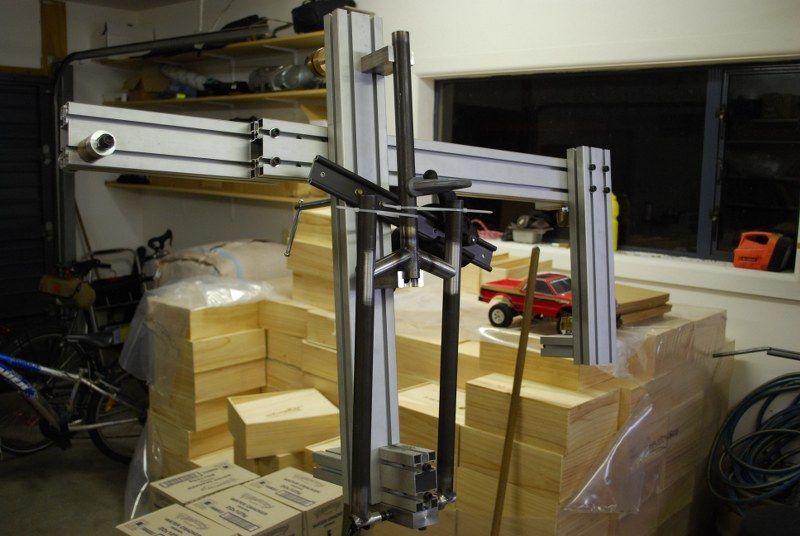
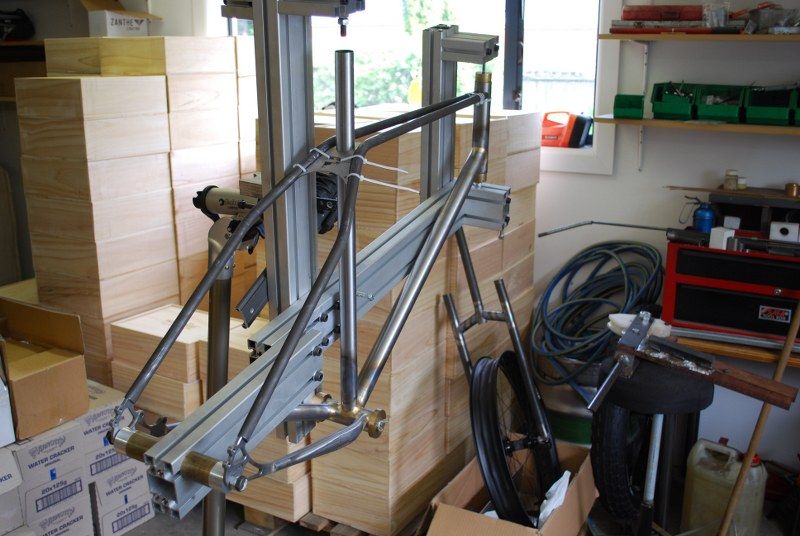
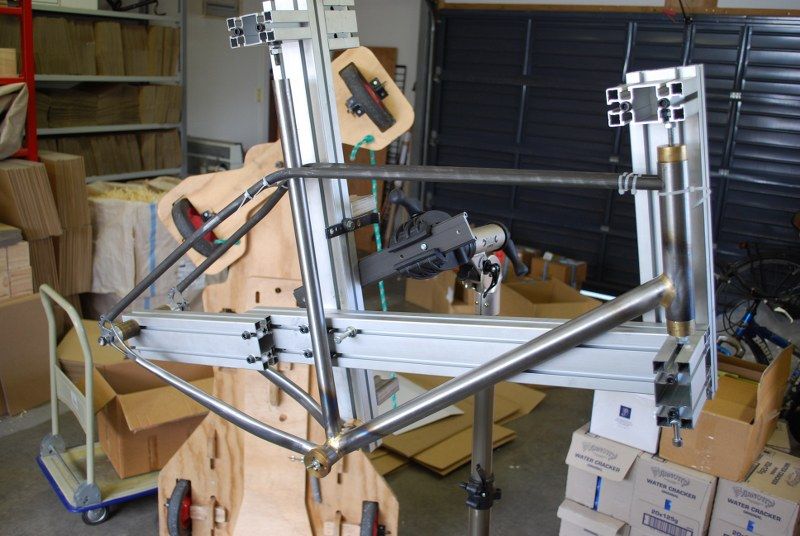
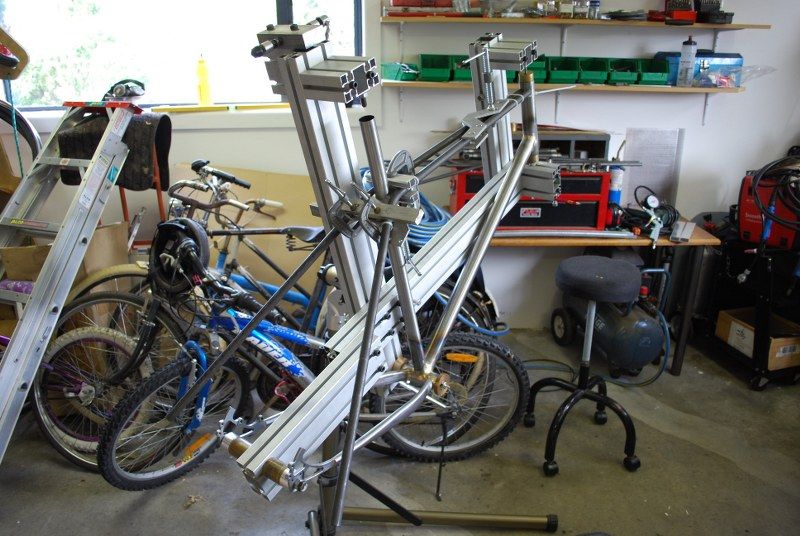
Having done most of the brazing on the frame, it is worth making a few notes on how the jig actually performed. Overall it does the job pretty well, but there are a few things that were less than satisfactory;

 - Generally I did the brazing in place on the jig, and one thing I noticed is that the big chunks of brass absorb quite a lot of heat. I kind of expected this to happen, but it made getting enough heat into the joint problematic at times.

 - Access to the side of the joint close to the jig was difficult, but because it tended to be the last bit you did things were already up to heat, so were still relatively easy to do. Whether brazing the nearside and then the farside of every joint is a good thing for making a totally straight frame is a question, but I tried to keep the brazing start points balanced where I could.

 - Once I had the main triangle and chainstays in place it was virtually impossible to remove the frame from the jig - I removed the fitting that holds the top of the seat tube, but even then it was hard. I will probably change things to improve this for the next frame.

Overall it worked pretty well though; 7 out of 10, should pay more attention in class. Story of my life really.


The lug brazing itself I am not 100% happy with to be honest, maybe I am being too hard on myself, but I felt I was getting things hotter than I really wanted in my efforts to get silver to wick into some of the joints. The simple ones with essentially the same pipe/lug material thicknesses were ok (the head tube joints for instance), the dropout joints were not too bad either, but the ones with complicated geometry and a long wicking path were pretty stressful to achieve; the seat lug, fork crown, chainstays into bottom bracket.

I think I have enough silver in there for it to not be a problem functionally, but the bit of me that wants each joint to be a thing of total beauty created with a zen like sense of competency and completeness is displeased. Still, it is my first frame, and it is all about the learning isn't it?

Anyway, soon I shall pop out soon to the ever helpful Bob, and we shall do the prep type work ie cleaning up the bottom bracket threads, reaming the seat tube, reaming the head tube and seating the fork crown bearing race.